Engineering the Future of
Empowering food businesses through Food Science, Technology, AI, Smart Manufacturing and Innovation to achieve sustainable growth and operational excellence.
Explore Our ServicesWhere Food Science Becomes Commercial Growth
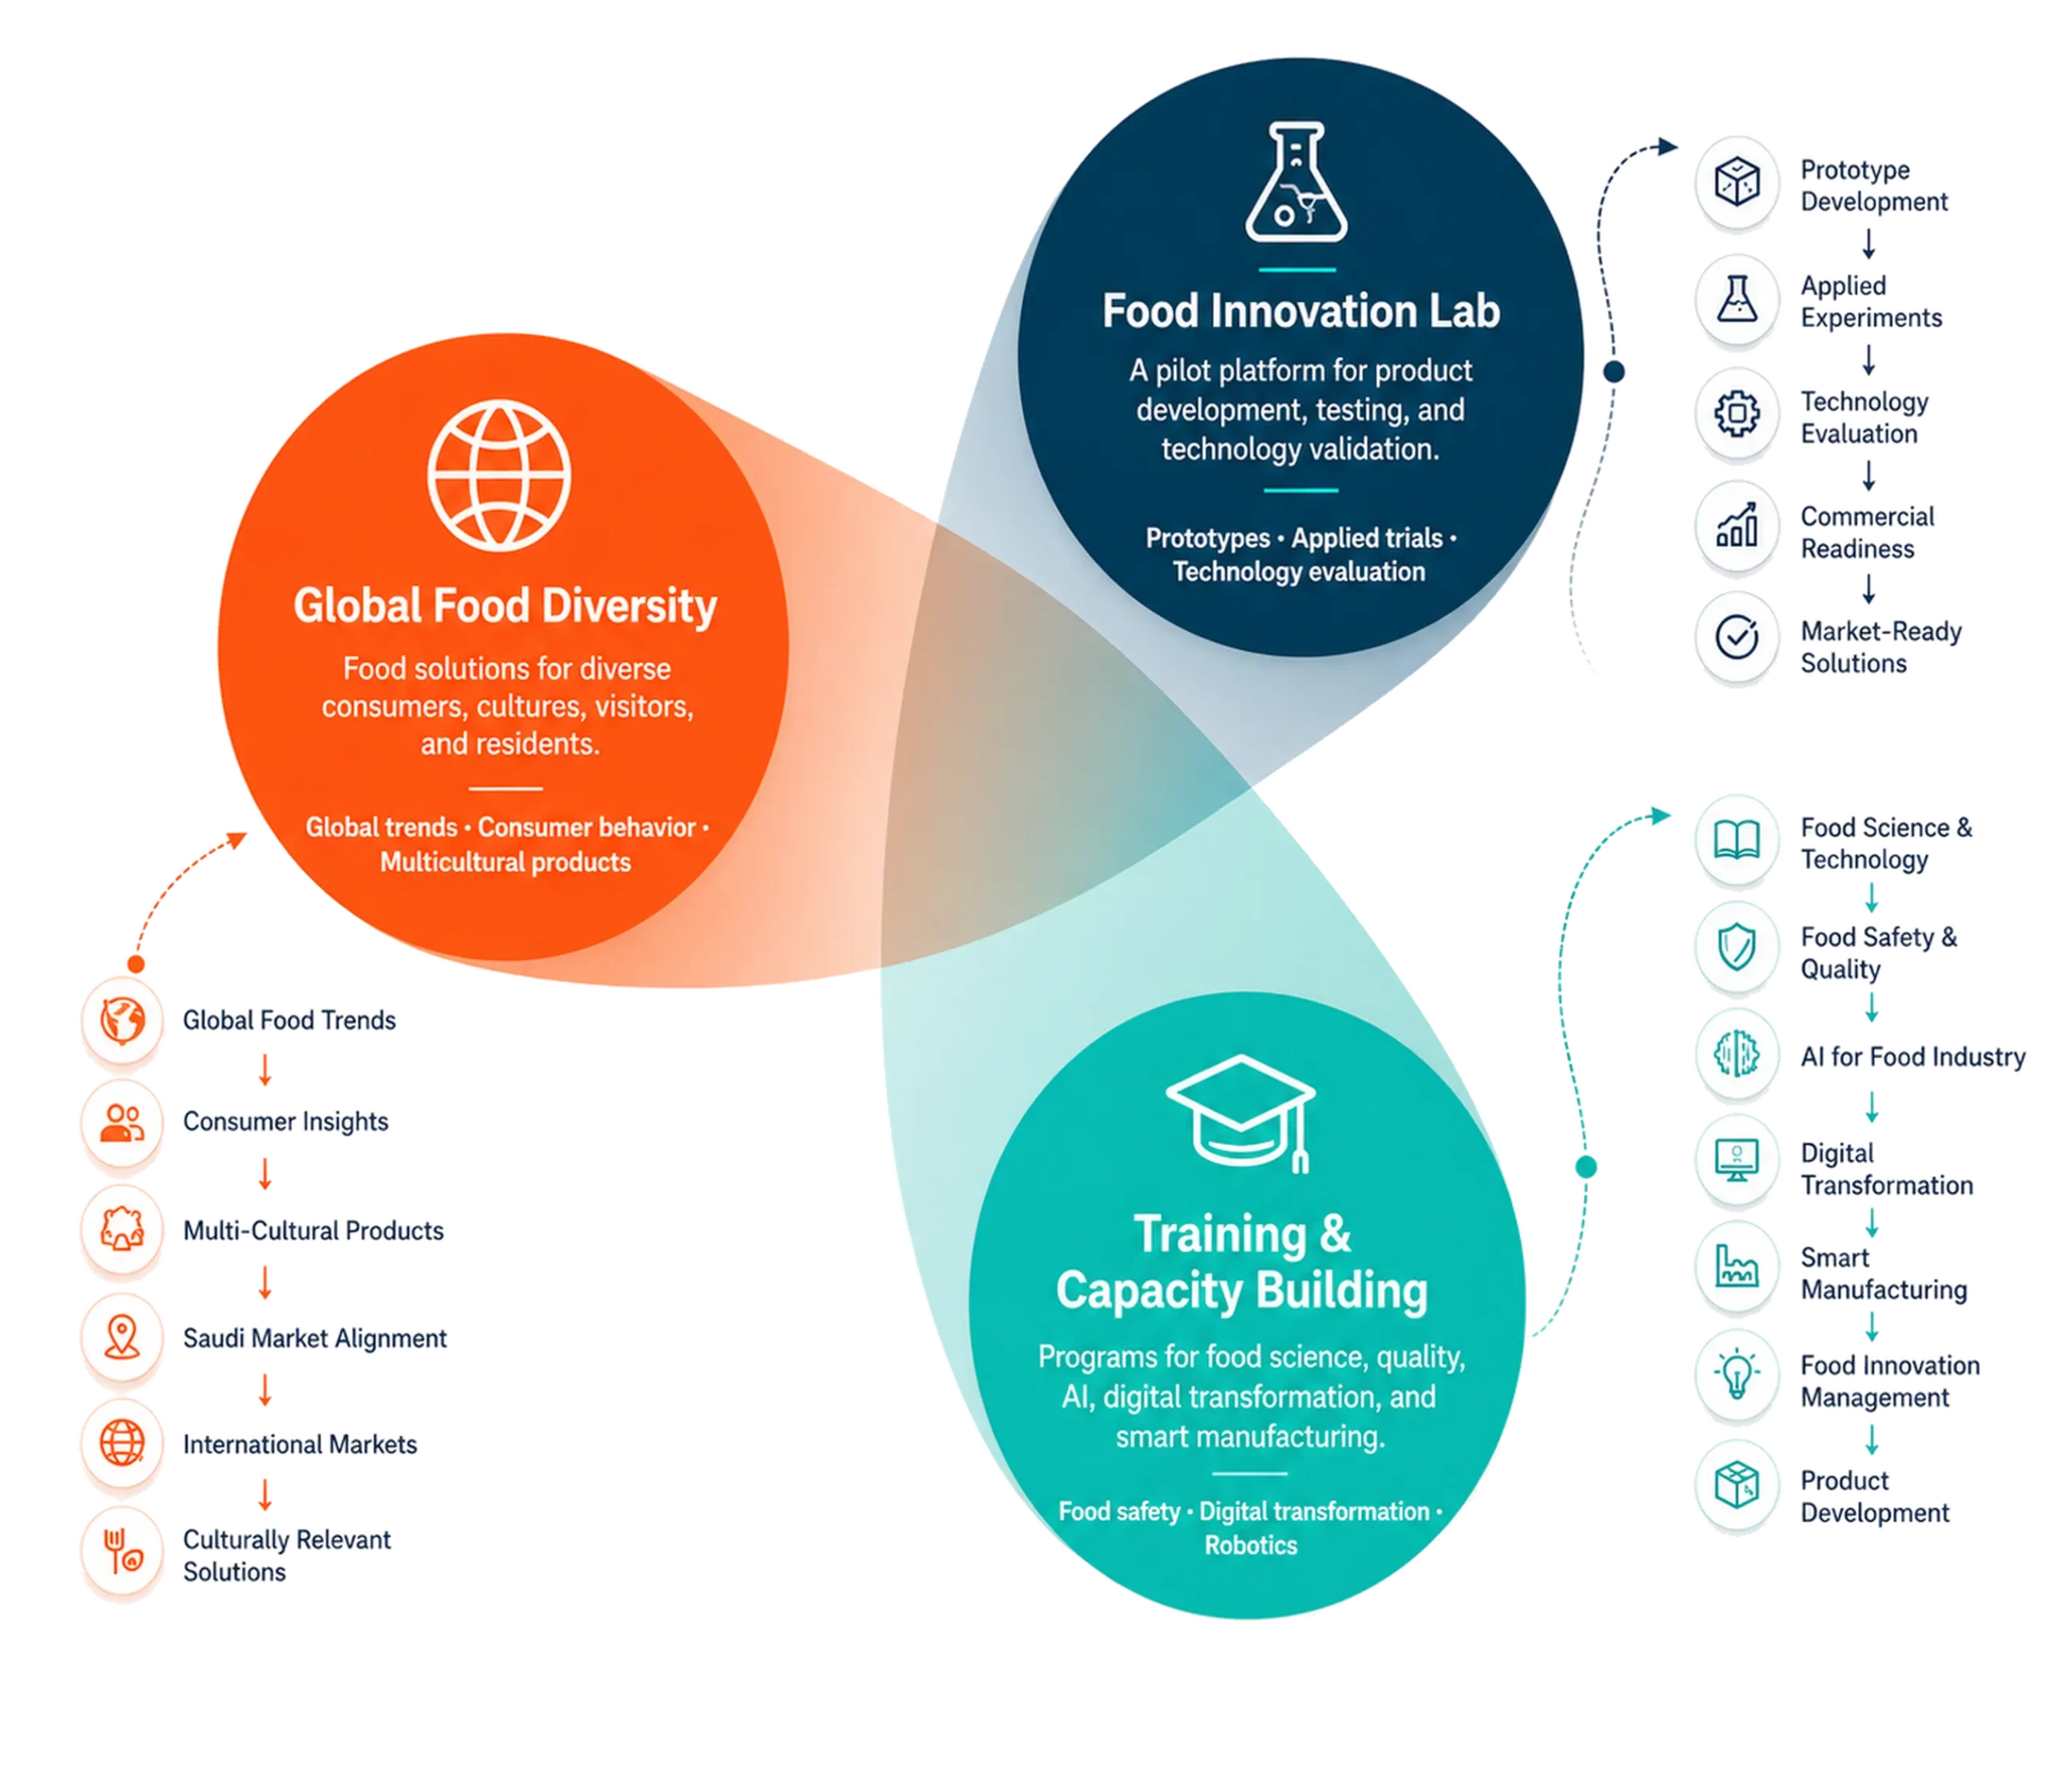
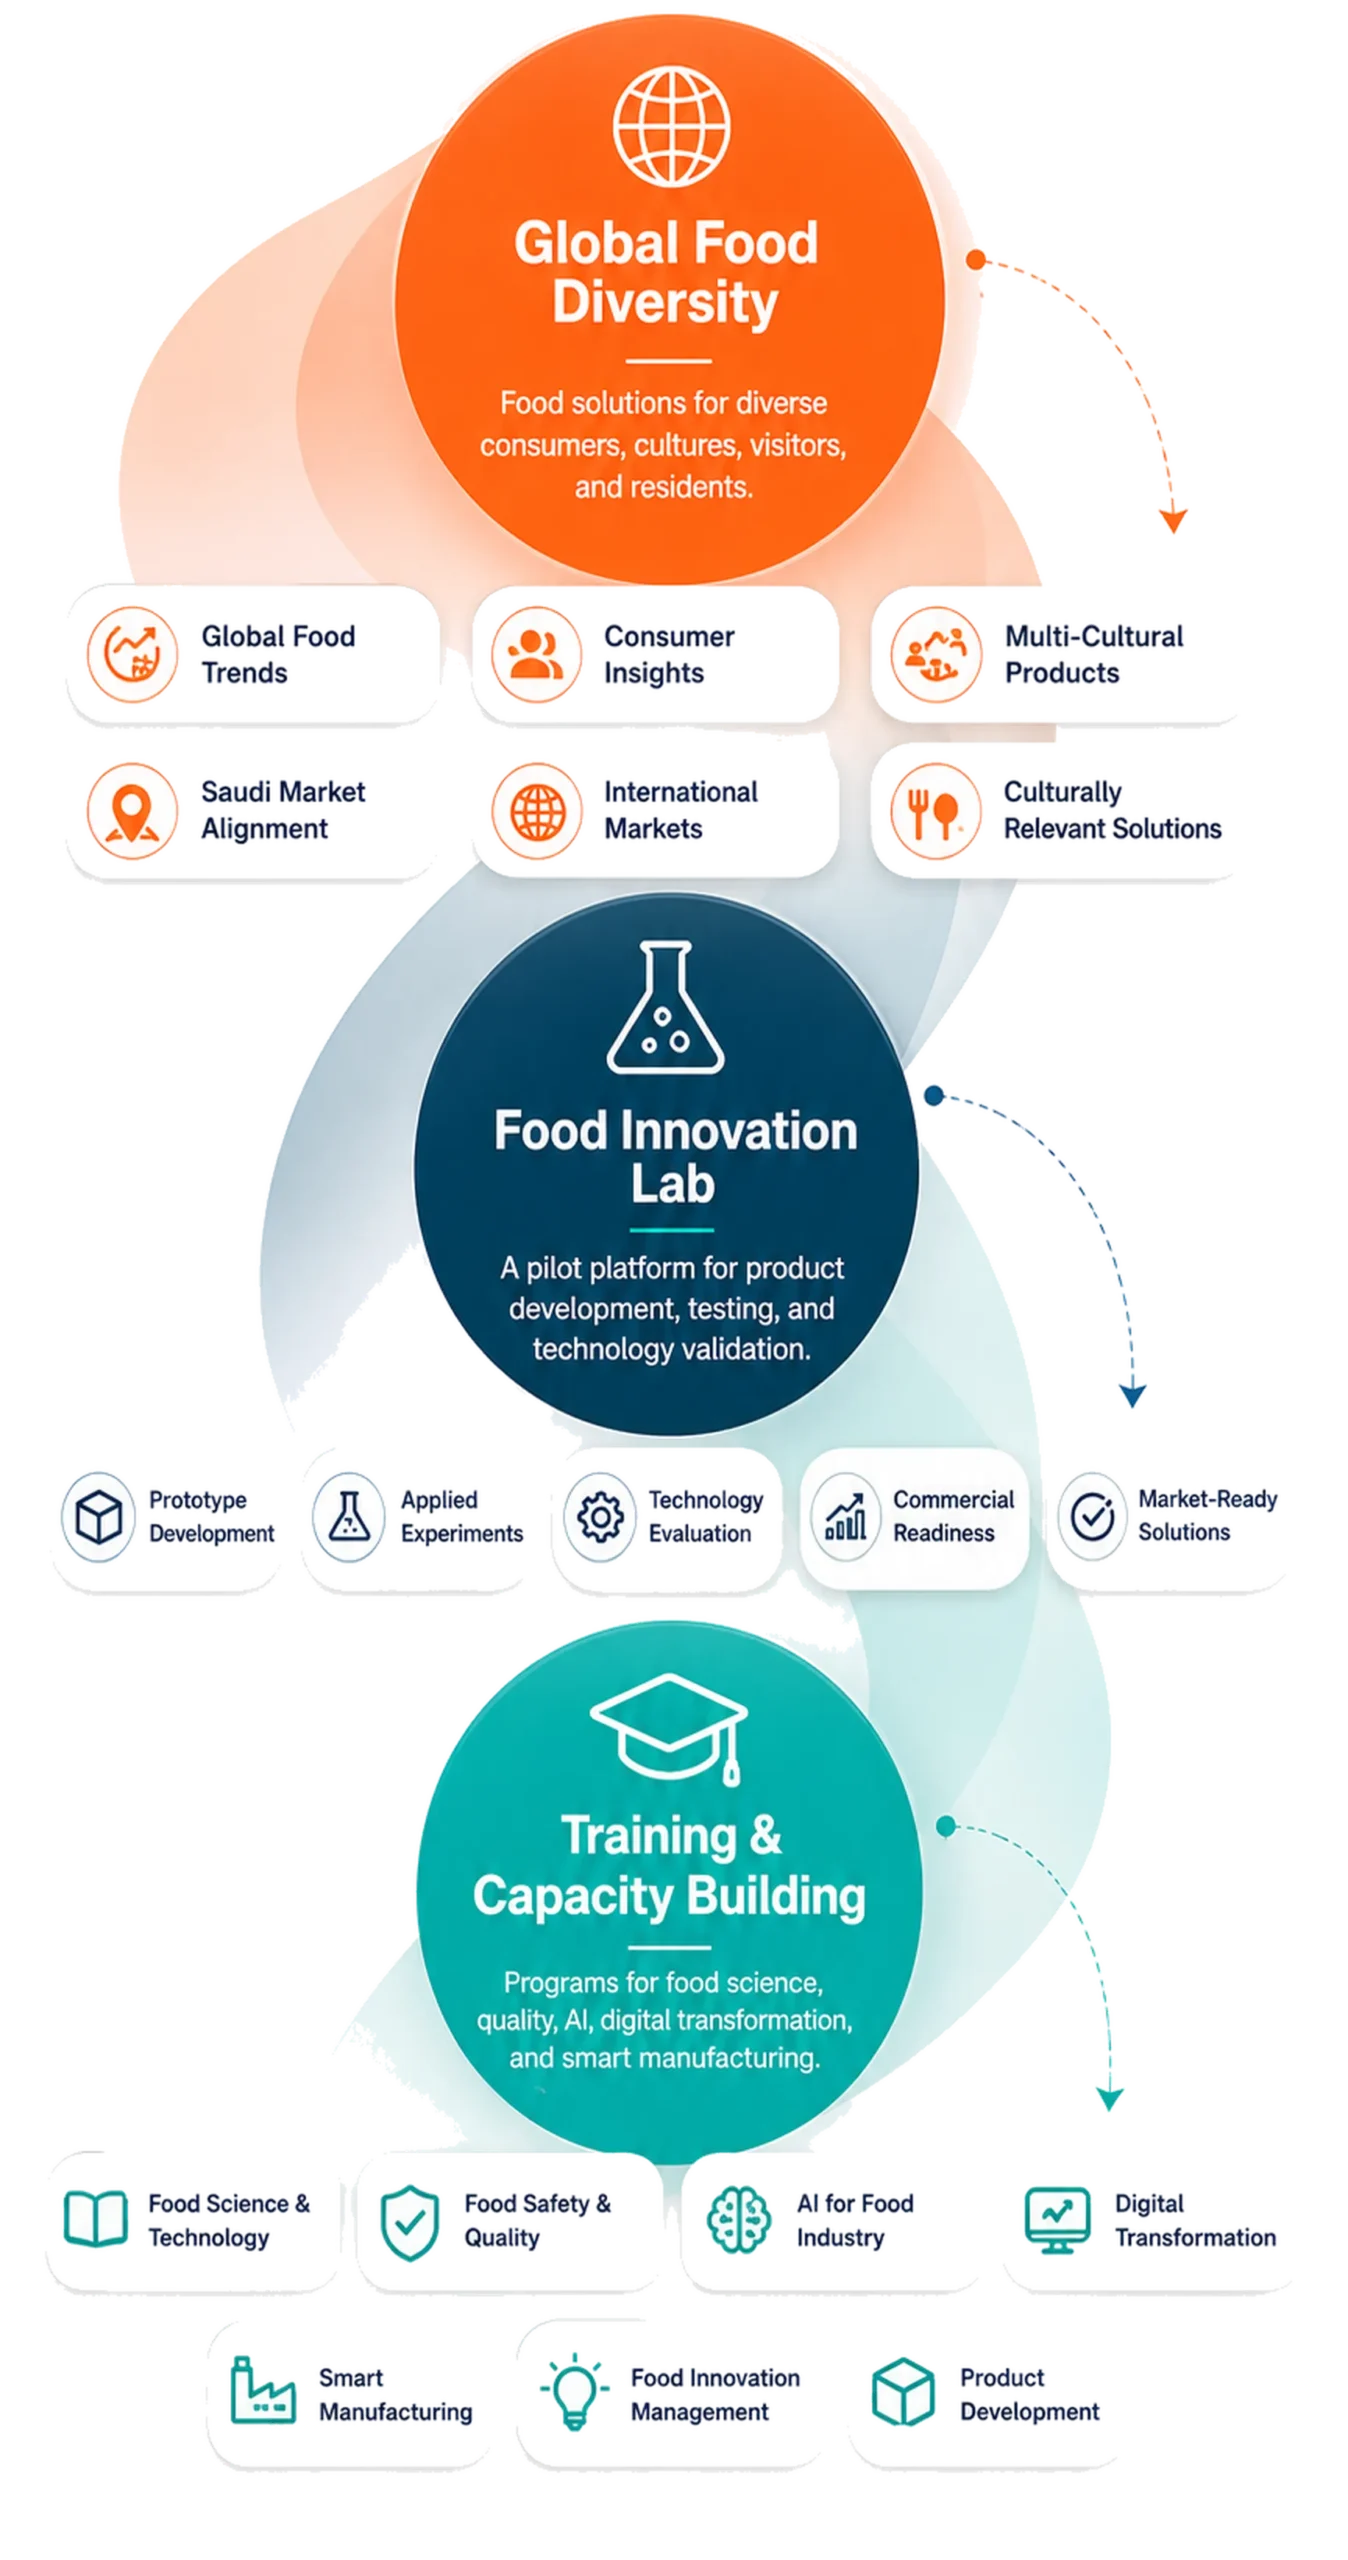
From Food Science to Smart Manufacturing
Integrated services that connect product science, safety, innovation, digital systems, and factory automation into one food-industry growth platform.
Food Science & Technology
Developing advanced food products through science, formulation, packaging, and commercial readiness.
- New Product Development
- Product Improvement
- Industrial Recipes
- Packaging Solutions
- Export Readiness
- Value-Added Products
Food Innovation
Creating innovative food concepts aligned with market trends, consumer needs, and scalable product opportunities.
- Food Concepts
- Prototype Development
- Consumer Insights
- Trend Analysis
- Innovation Support
- Commercialization
Food Safety & Compliance
Helping food businesses apply global safety systems and meet Saudi regulatory and audit requirements.
- HACCP
- ISO 22000
- FSSC 22000
- GMP
- Quality Programs
- SFDA Compliance
AI & Smart Manufacturing
Applying AI inside real food operations to improve quality, safety, traceability, and production performance.
- Computer Vision
- Predictive Analytics
- Cold Chain
- Quality Data
- Traceability
- Process Optimization
Digital Transformation
Digital systems for modern food factories, connecting data, quality, operations, and decision-making.
- ERP
- MES
- QMS
- LIMS
- IoT
- Analytics Dashboards
Technology Transfer
Transferring and implementing modern technologies inside food production environments.
- Technology Evaluation
- Factory Solutions
- Implementation
- Training
- Knowledge Transfer
- Smart Manufacturing
Industrial Robotics
Automation solutions for efficient food production, packaging, quality control, and operational safety.
- Industrial Robots
- Automation
- Quality
- Safety
- Traceability
- Packaging Lines
Industries We Serve
Specialized support for food businesses across key manufacturing sectors, helping each client see that ELAF understands their specific industry.
- Dairy
- Bakery
- Chocolate & Confectionery
- Meat & Poultry
- Beverages
- Snacks
- Ingredients
- Food Manufacturing
Specialized Support Across Food Manufacturing Sectors
ELAF works with food businesses across key industry categories, helping each client find solutions tailored to their products, operations, and market needs.
Meat & Poultry
Processed meat, poultry products, quality, safety, and formulation.
Chocolate & Confectionery
Chocolate, sweets, fillings, textures, flavors, and product innovation.
Bakery
Bread, pastries, baked goods, shelf life, and production optimization.
Dairy
Milk, yogurt, cheese, and chilled dairy product development.
Snacks
Savory snacks, healthy snacks, flavors, coatings, and new formats.
Ingredients
Food ingredients, blends, additives, functionality, and applications.
Beverages
Juices, functional drinks, hot and cold beverages, and stability.
Food Manufacturing
Factory operations, process improvement, quality systems, and scale-up.
Proven Impact Across Food Industry Projects
Even when client names remain confidential, the results tell the story. ELAF supports food businesses through practical projects that improve products, operations, safety, cost efficiency, and technology readiness.
Product Development Projects
From concept to prototype and commercial-ready food products.
Production Cost Optimization
Improving process efficiency, raw material usage, and operational cost structure.
Shelf-life Improvement
Enhancing product stability, packaging performance, and market readiness.
Food Safety Implementation
Building practical systems aligned with HACCP, ISO 22000, FSSC 22000, GMP, and SFDA requirements.
Operational Excellence
Improving factory workflows, quality control, traceability, and production consistency.
AI Transformation Projects
Applying AI and smart systems to support quality, inspection, prediction, and decision-making.
A Food Industry Partner for Growth, Quality, and Transformation
ELAF Food Science & Technology helps food businesses turn ideas, products, operations, and technologies into scalable commercial outcomes across the Saudi and GCC food sector.
Product Development
We develop new food products, improve existing formulas, and build industrial recipes ready for production.
Concept to Prototype
We transform food ideas and market trends into practical prototypes and value-added product concepts.
One connected model from food science to compliance, technology, and smart manufacturing.
Safety & Quality Systems
We support HACCP, ISO, FSSC, GMP, traceability, audits, and SFDA readiness for food businesses.
Smart Manufacturing
We apply AI, digital systems, technology transfer, robotics, and automation inside real food operations.
Why Businesses Choose ELAF
ELAF combines food science, innovation, compliance, AI, digital transformation, and smart manufacturing to help food businesses move from ideas to scalable, market-ready growth.
Understand
We study the product, market, consumer needs, and factory reality.
Develop
We build formulas, prototypes, recipes, and value-added food concepts.
Validate
We support quality, safety, compliance, testing, and audit readiness.
Integrate
We connect AI, digital systems, technology transfer, and automation.
Scale
We prepare products, brands, and operations for commercial growth.
Integrating Intelligent Technologies for Smarter Food Manufacturing
Frequently Asked Questions
Clear answers about how ELAF supports food businesses through science, innovation, compliance, technology, AI, and smart manufacturing.
Technologies We Work With
We select and apply modern technologies inside real food manufacturing environments to improve quality, traceability, efficiency, and commercial readiness.
ERP Systems
Business operations, inventory, procurement, finance, and production planning.
MES Systems
Manufacturing execution, line performance, production tracking, and process control.
QMS Systems
Quality workflows, corrective actions, inspections, audits, and compliance records.
A connected technology layer for food factories, labs, quality teams, supply chains, and management decisions.
LIMS Systems
Lab testing, sample tracking, food safety data, and quality validation.
IoT & Smart Sensors
Cold chain monitoring, equipment data, temperature, humidity, and line visibility.
AI & Computer Vision
Defect detection, quality analysis, risk prediction, and process optimization.